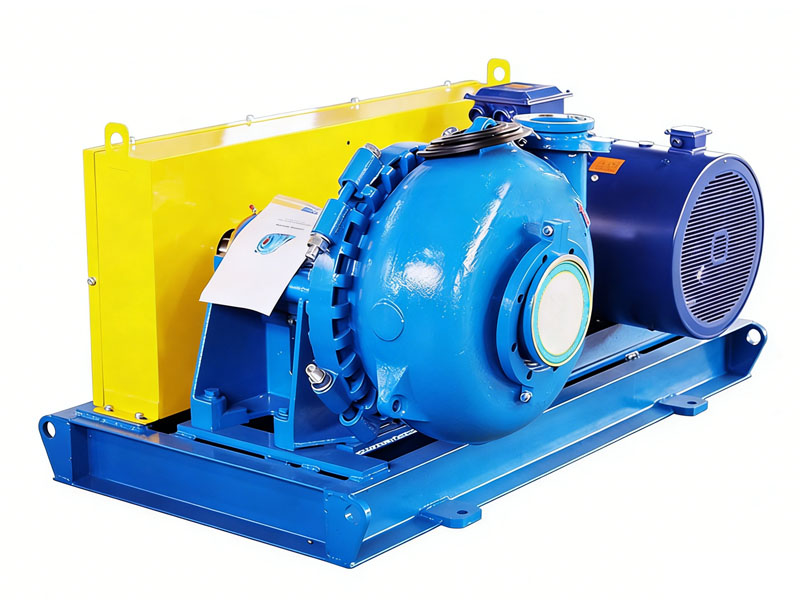

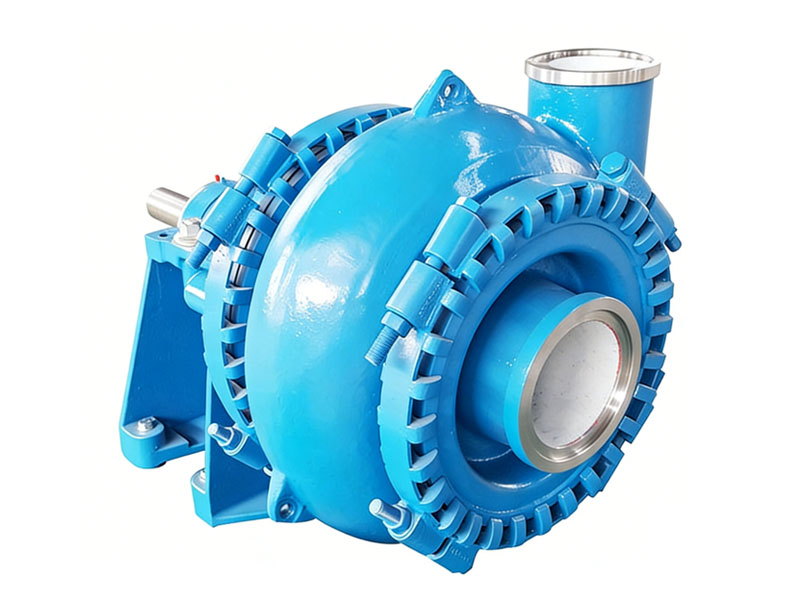
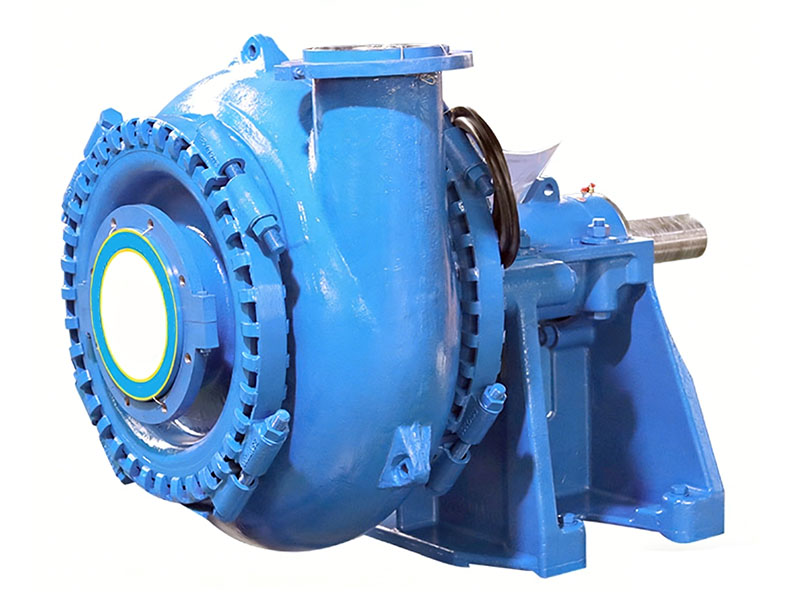
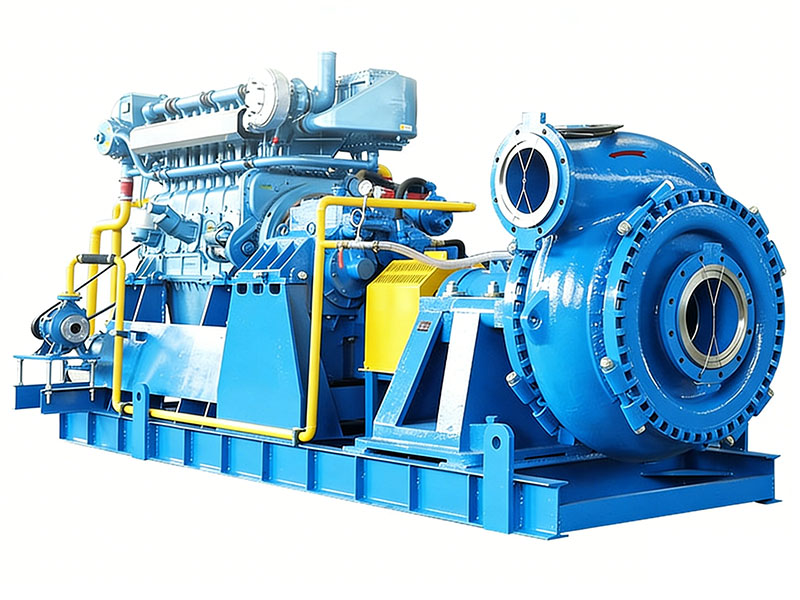
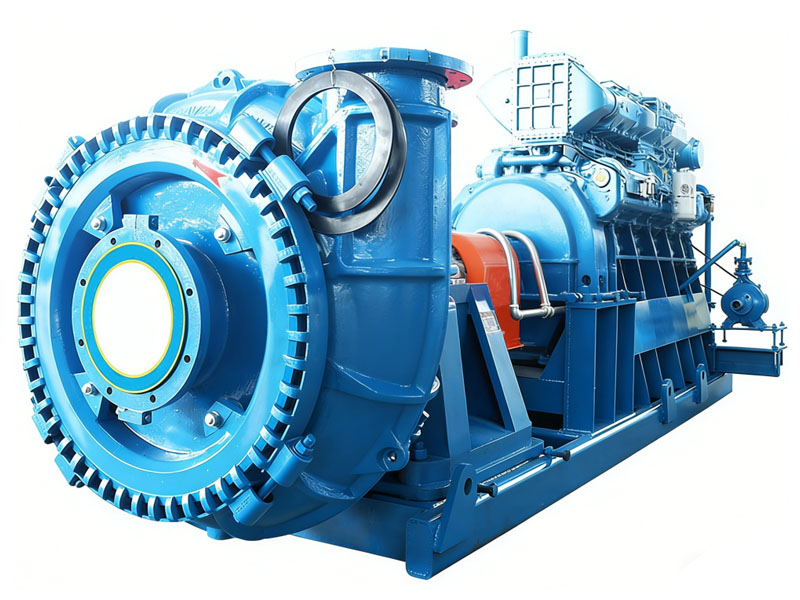
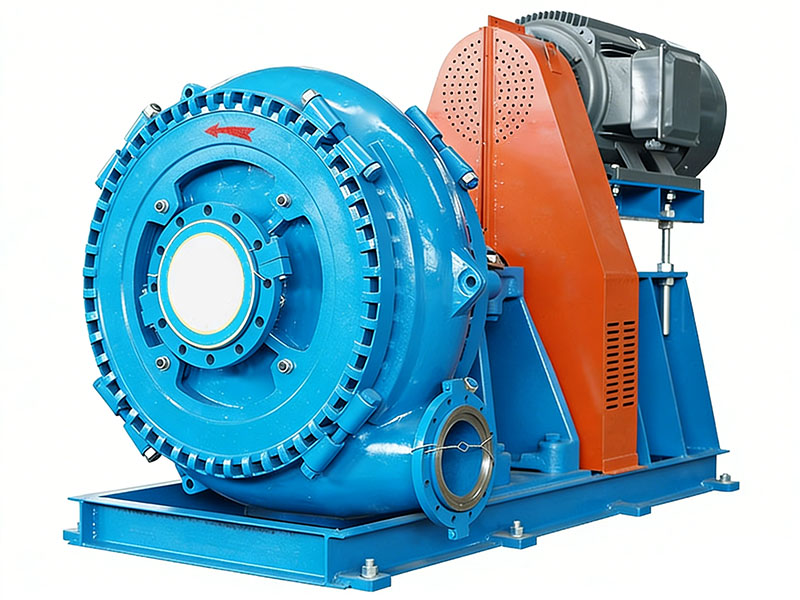
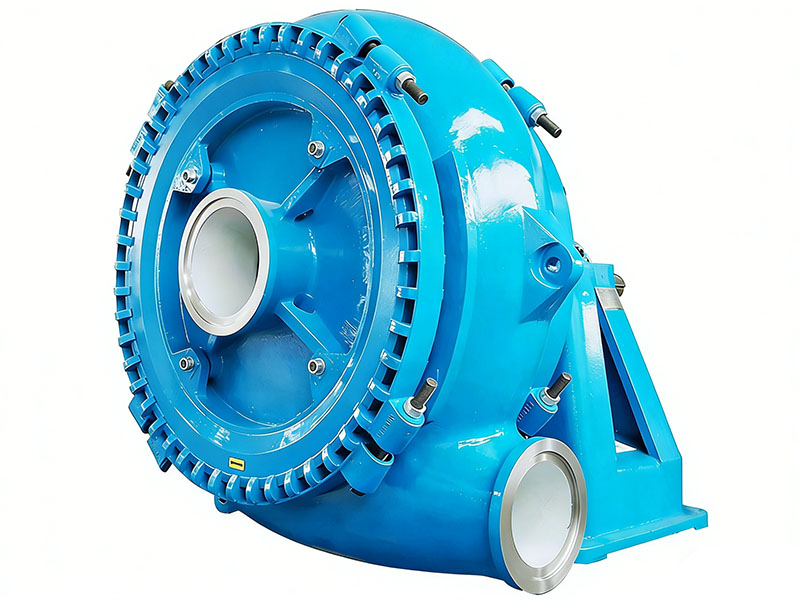
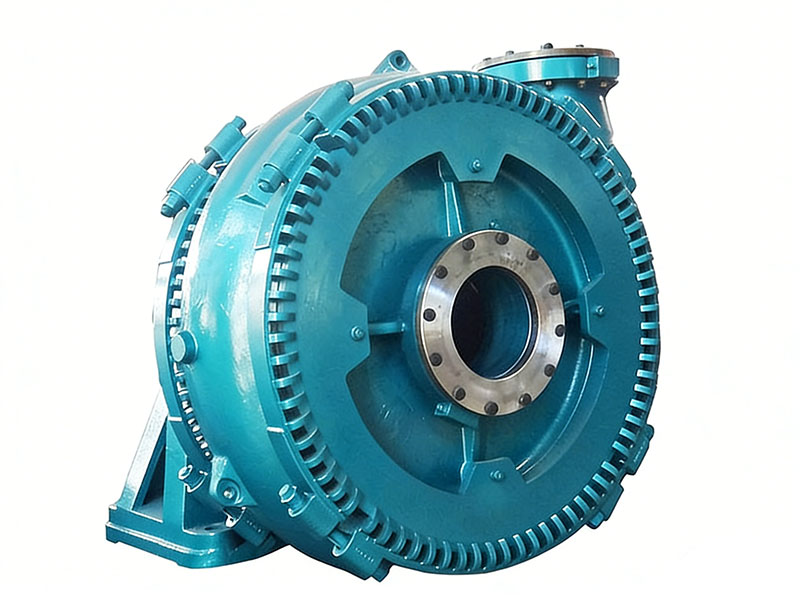
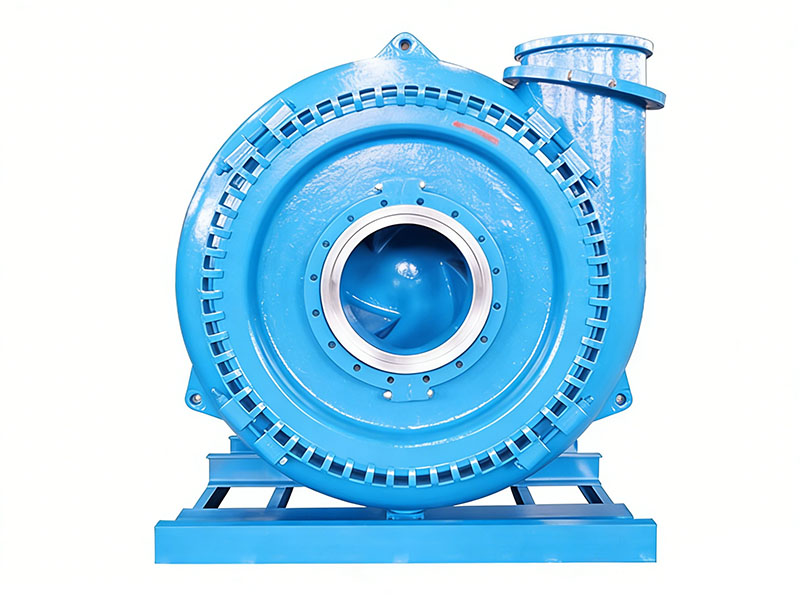
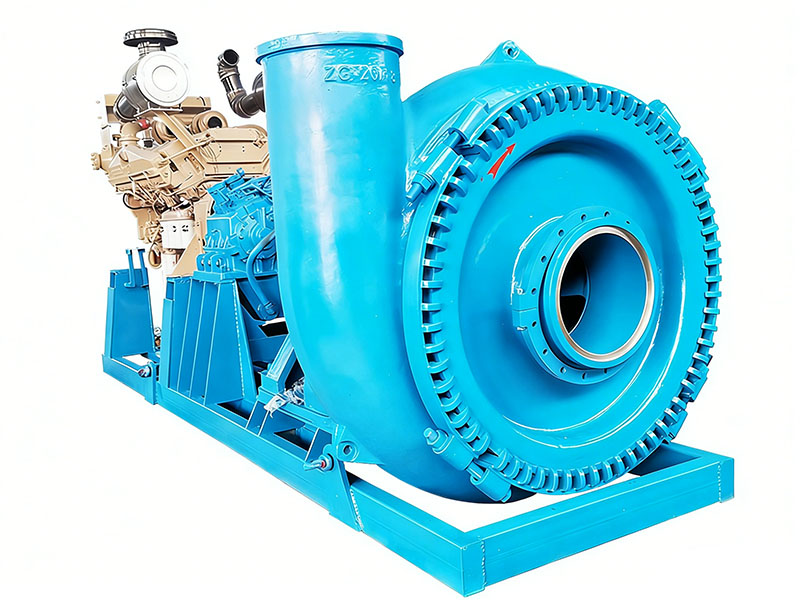
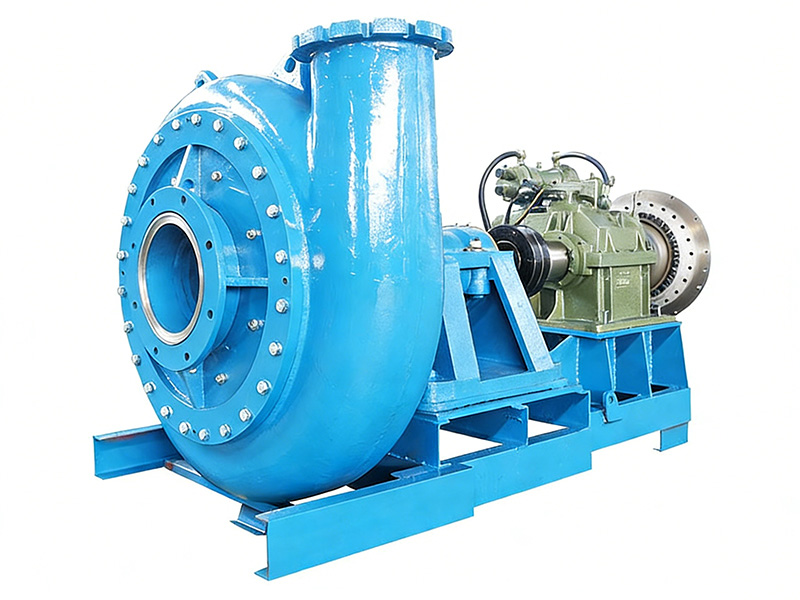
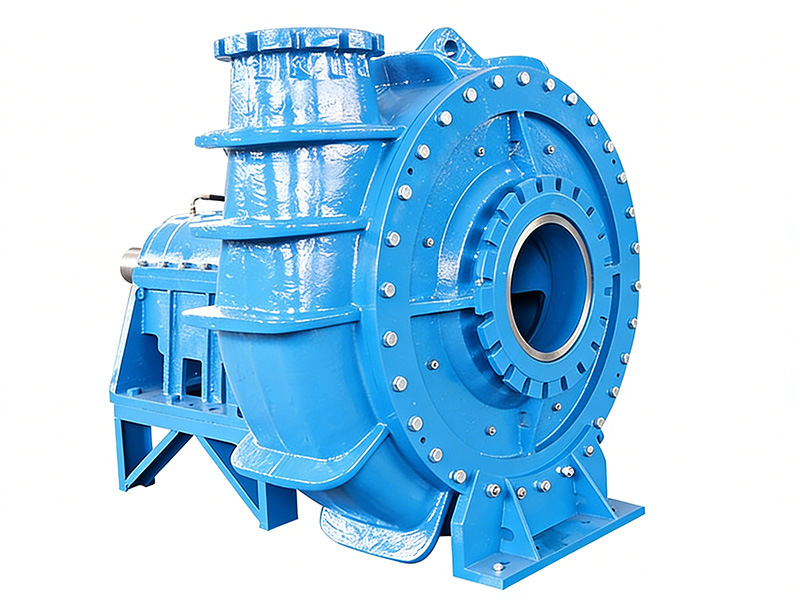
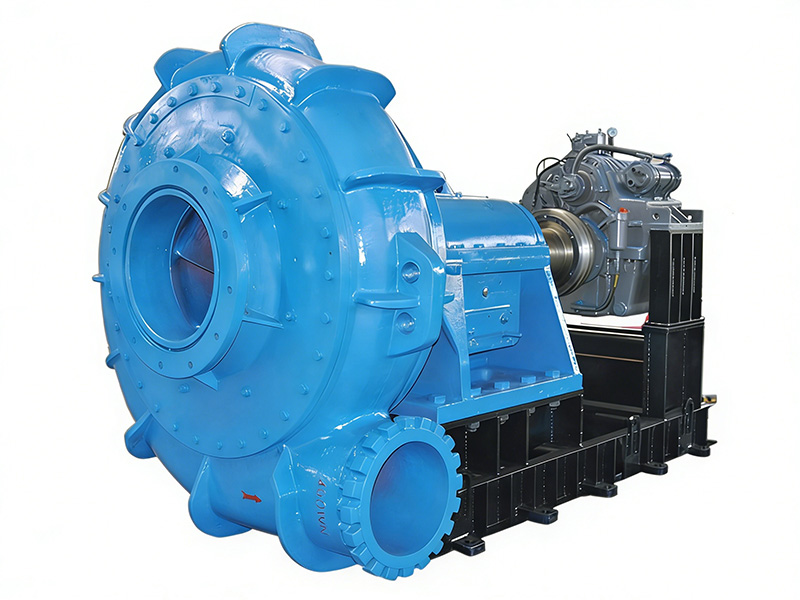
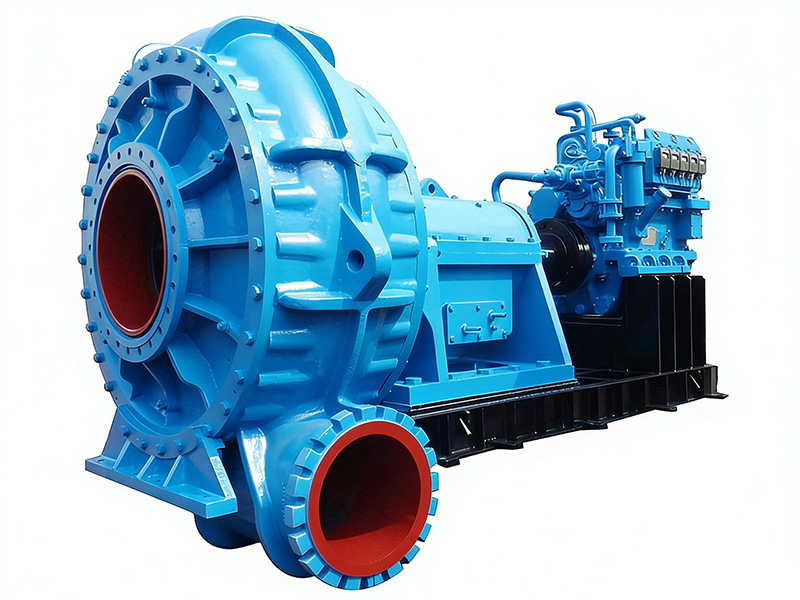
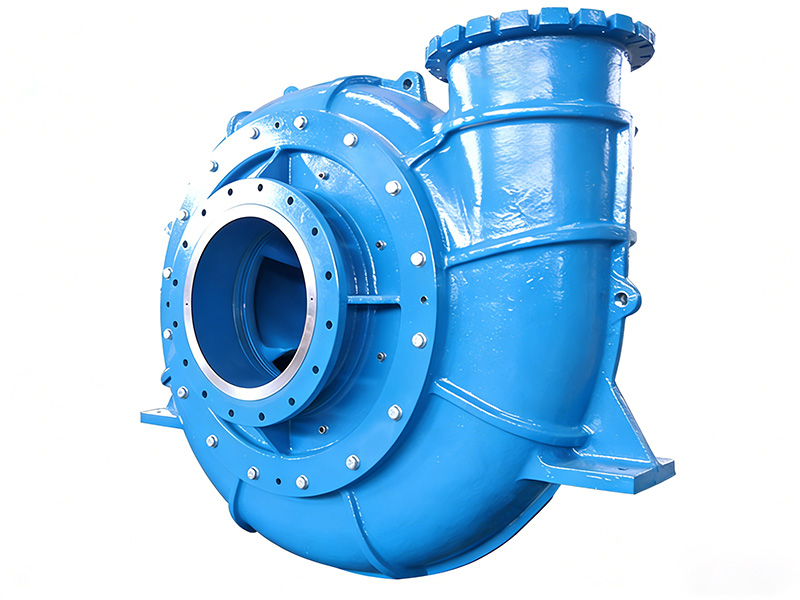
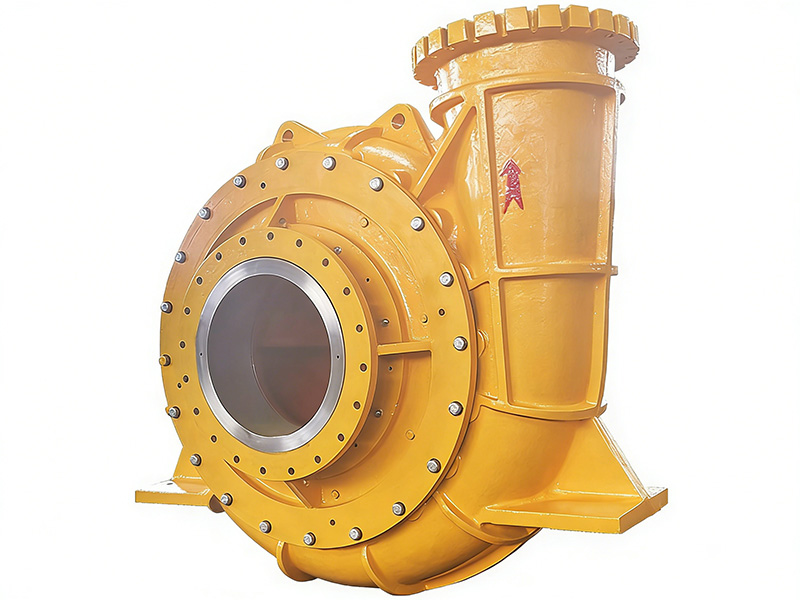
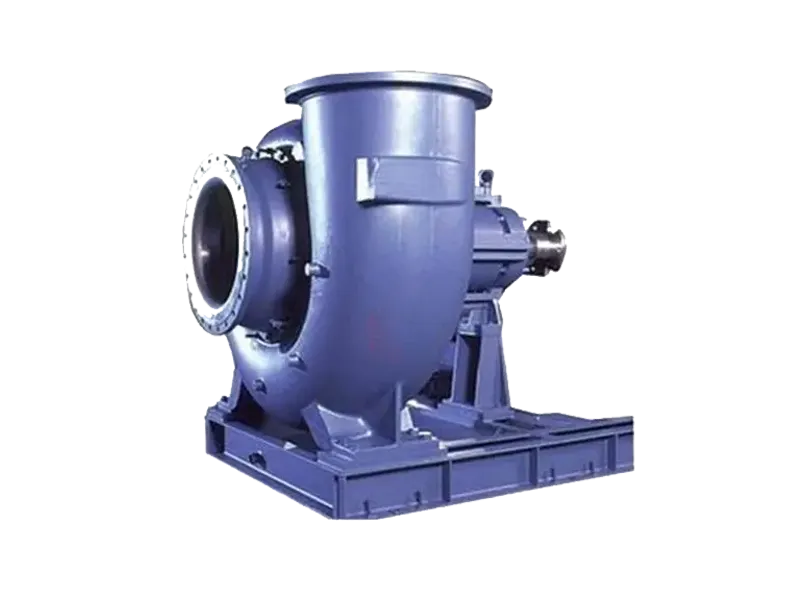
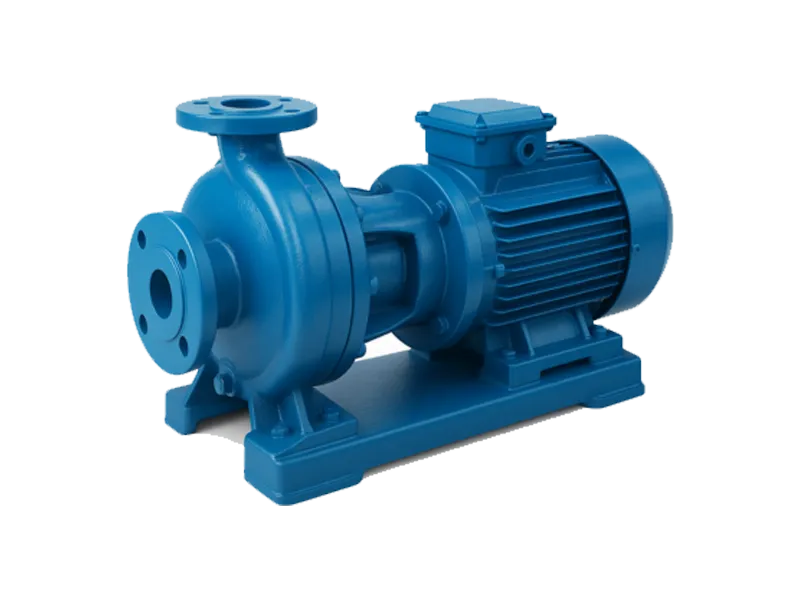
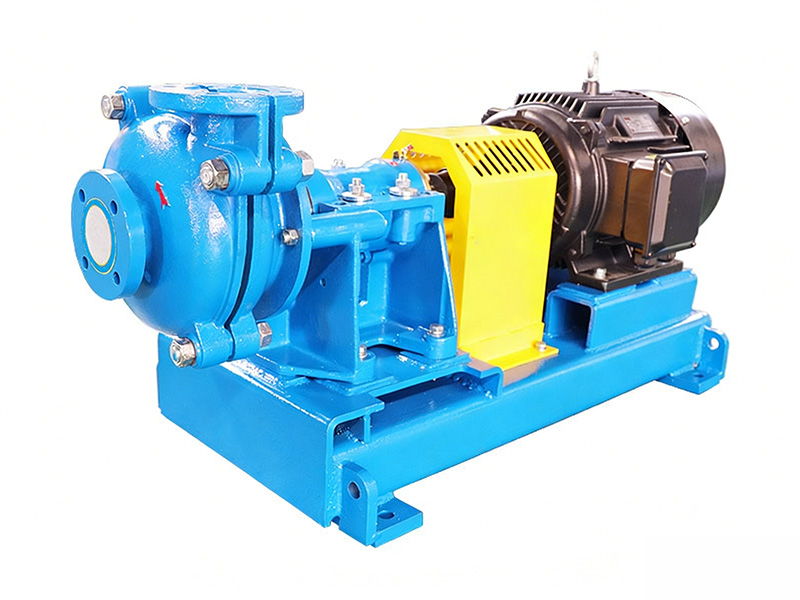
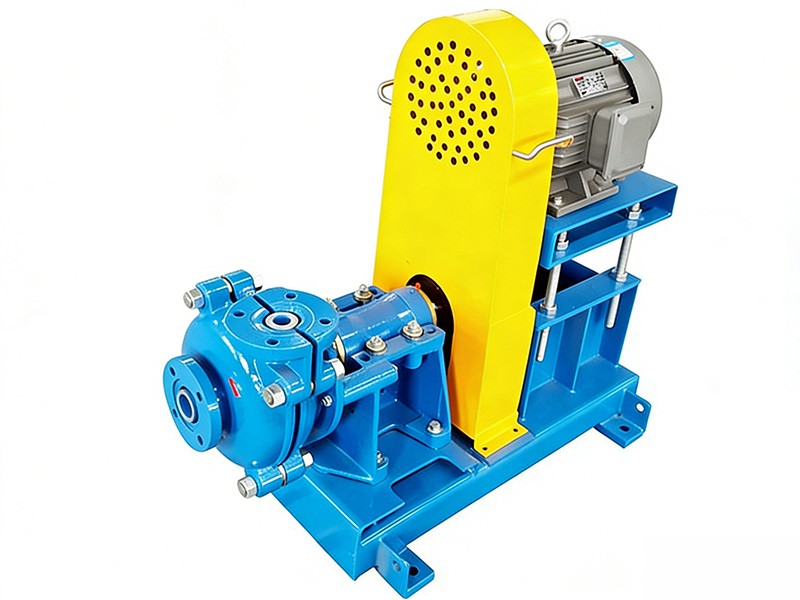
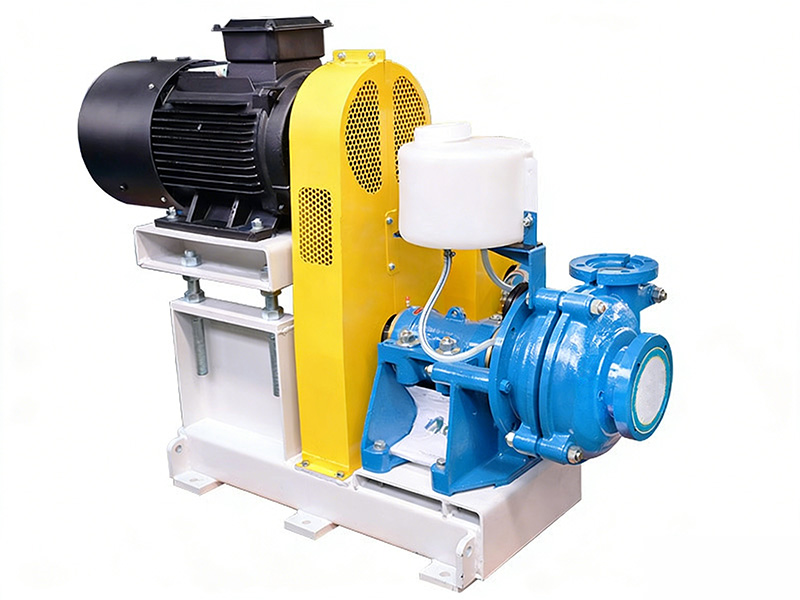
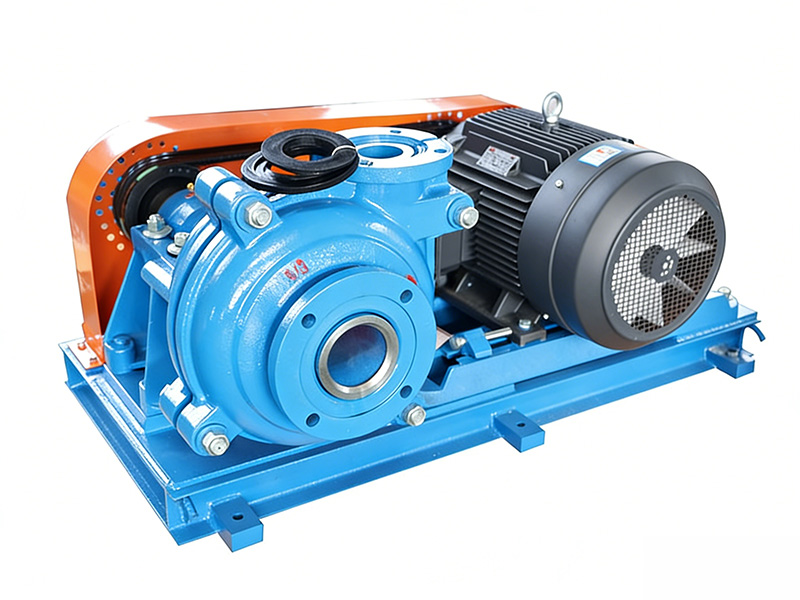
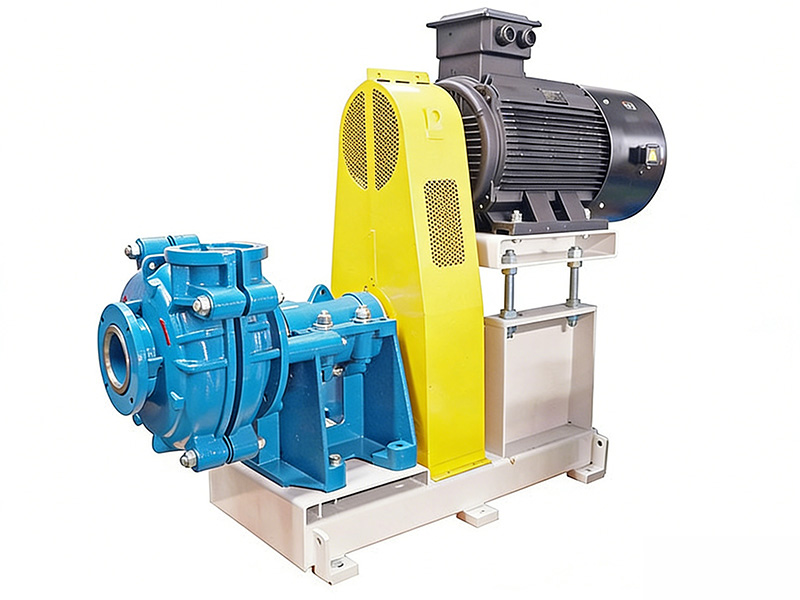
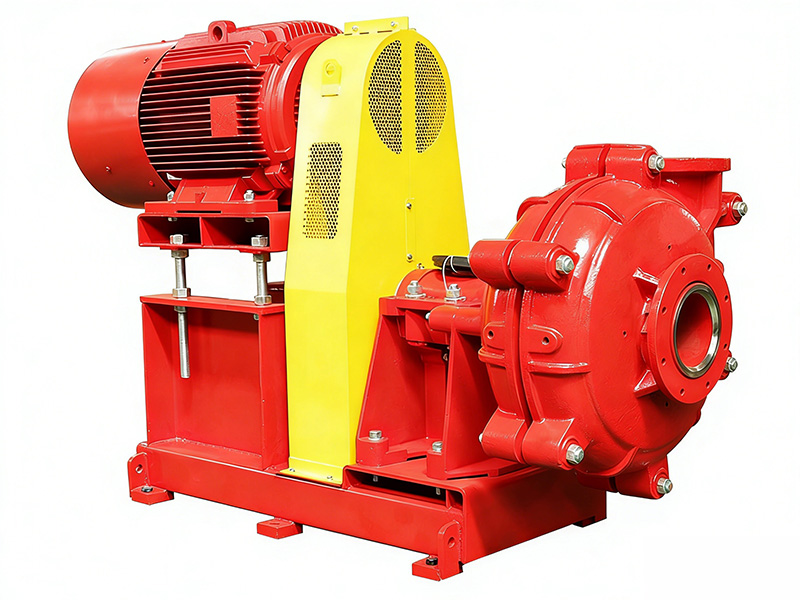
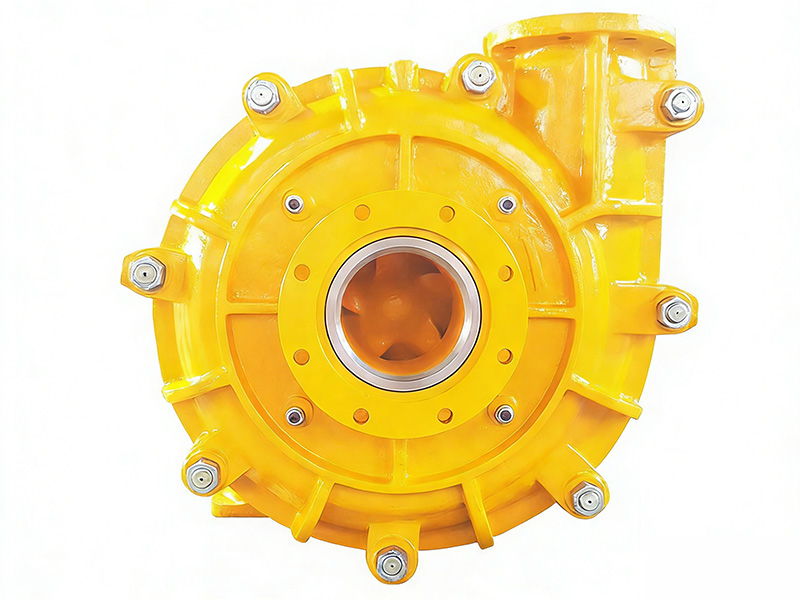
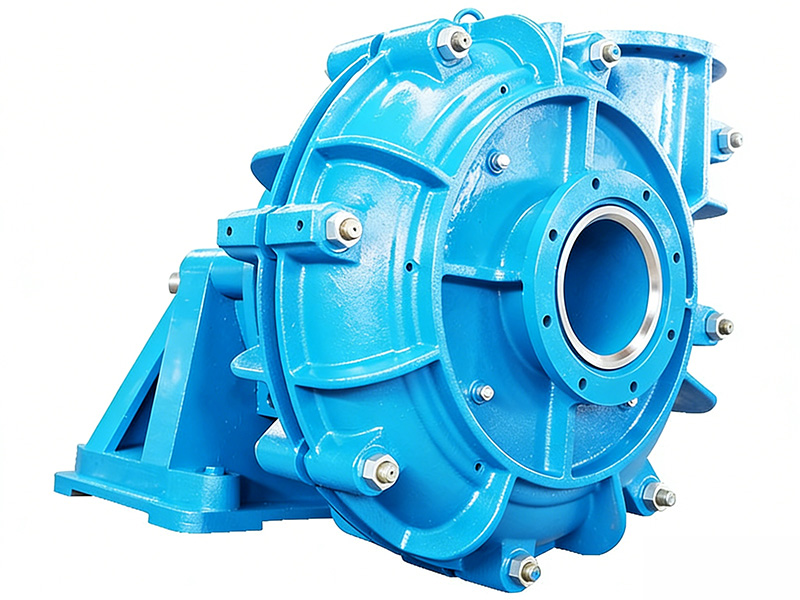
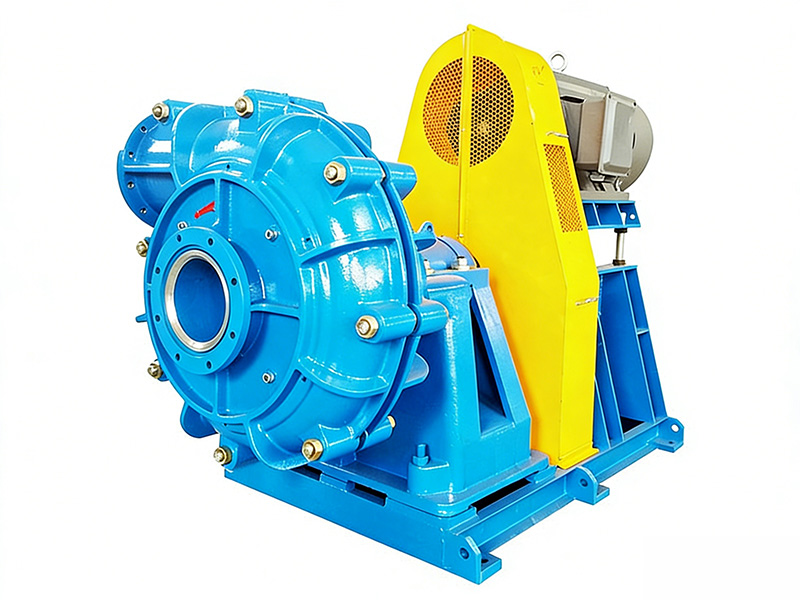
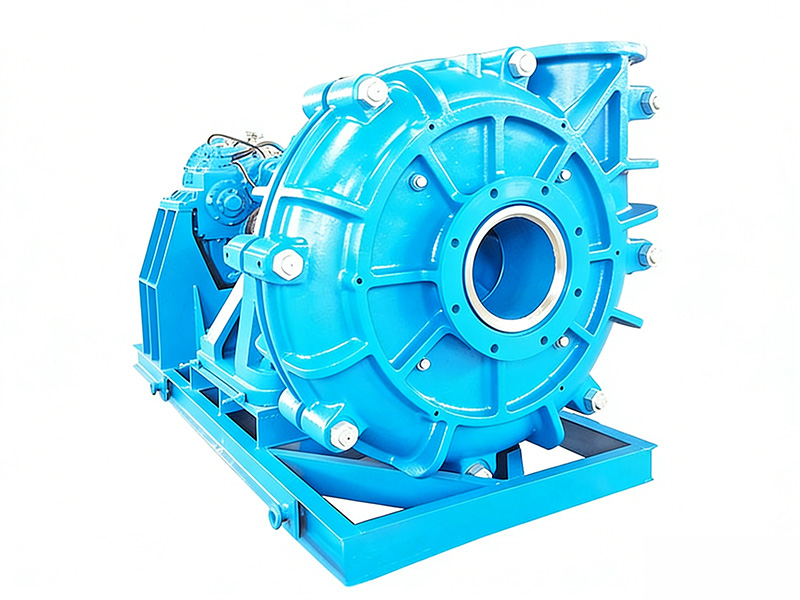
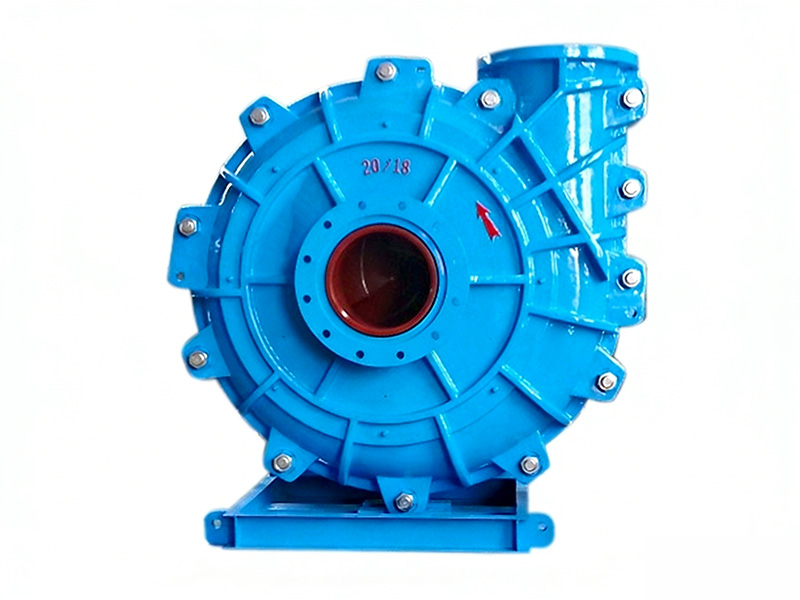
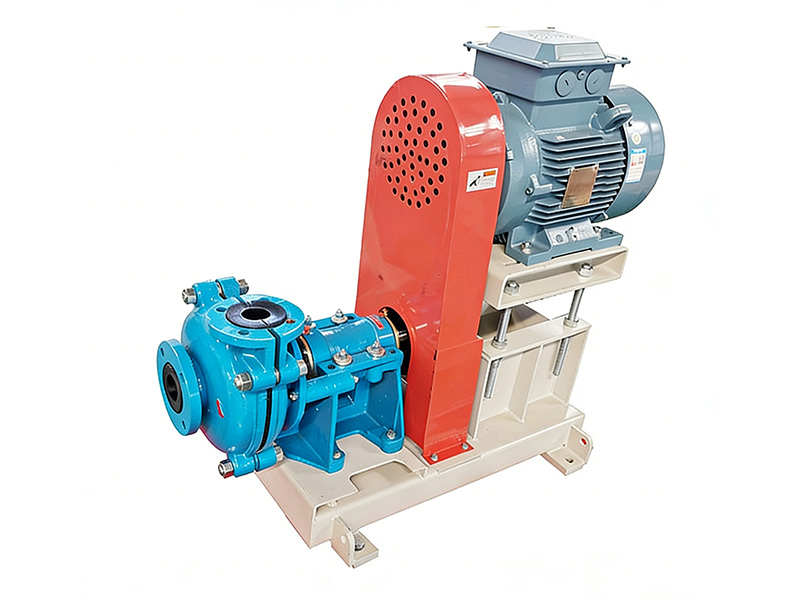
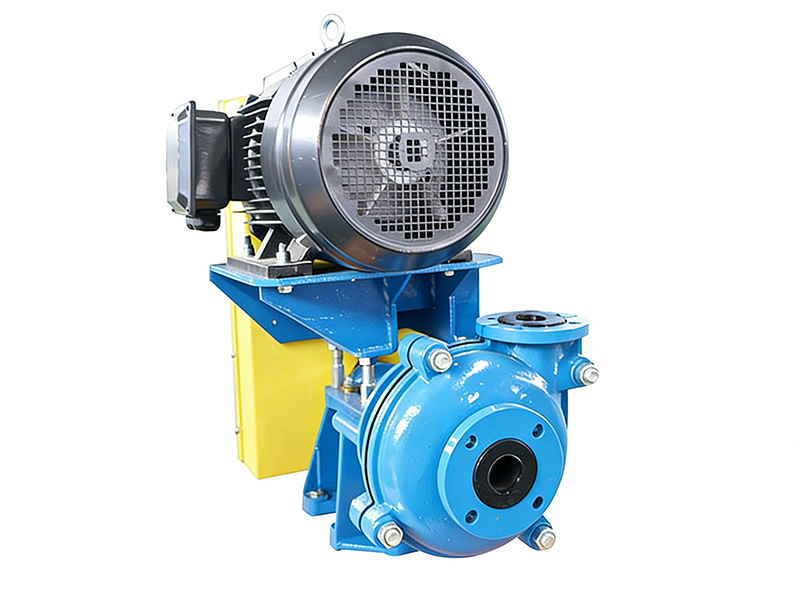
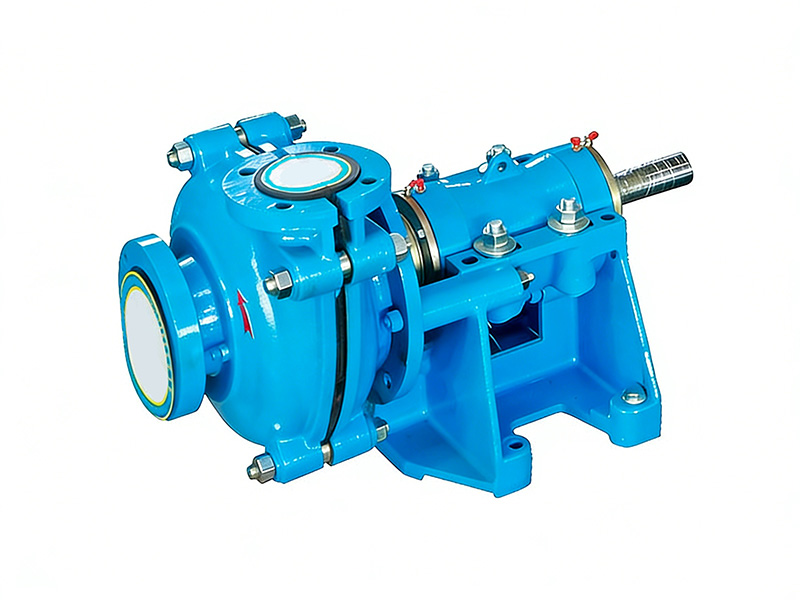
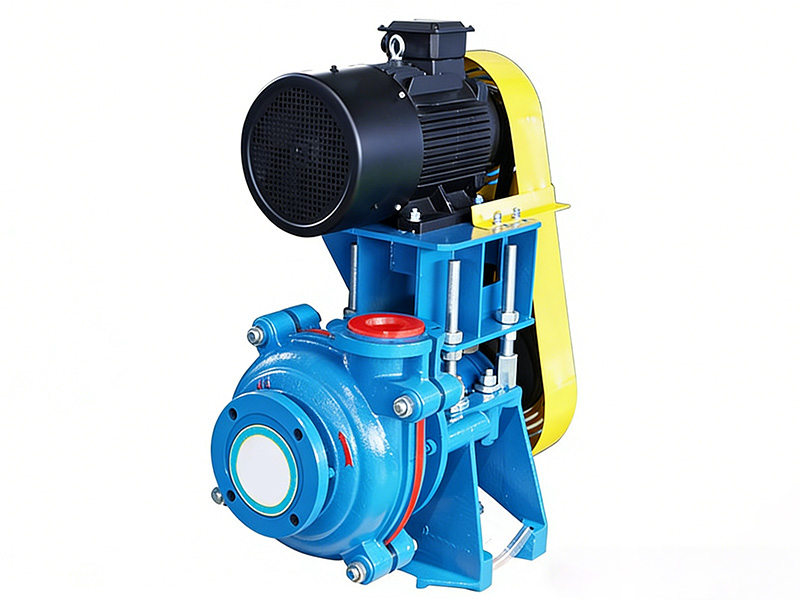
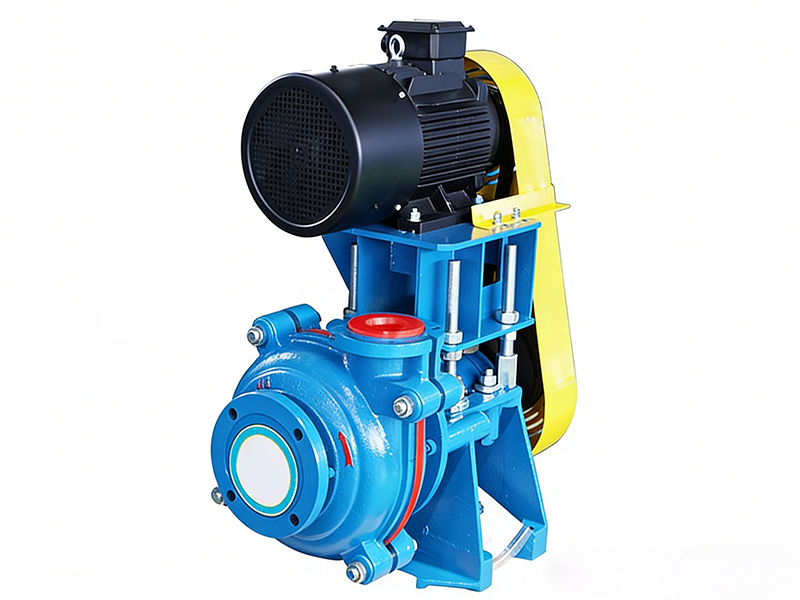
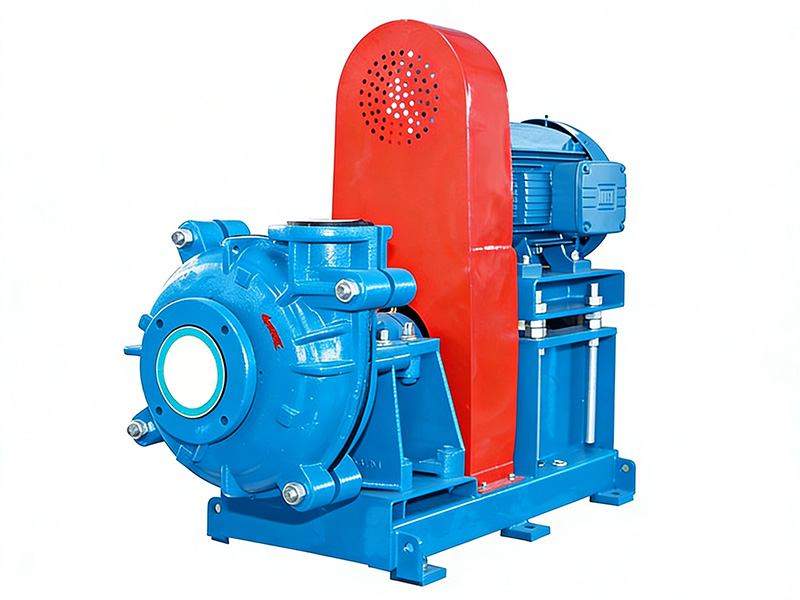
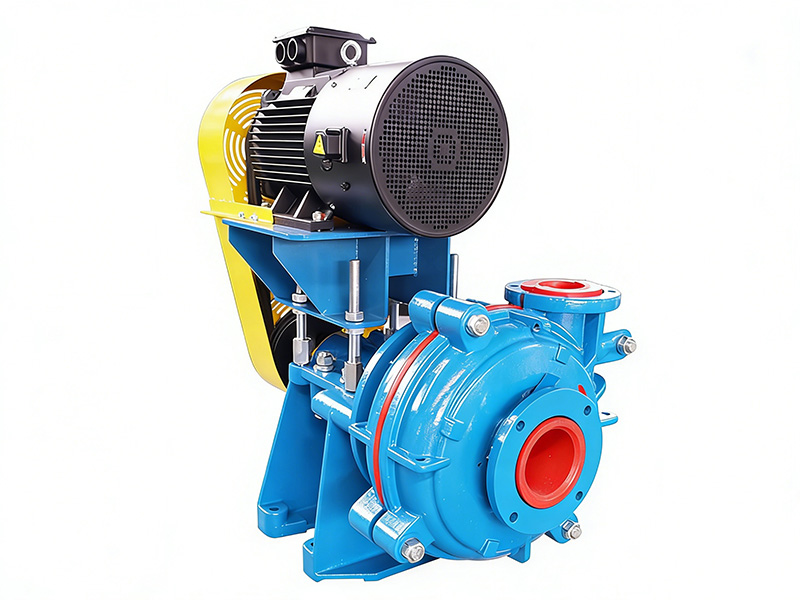
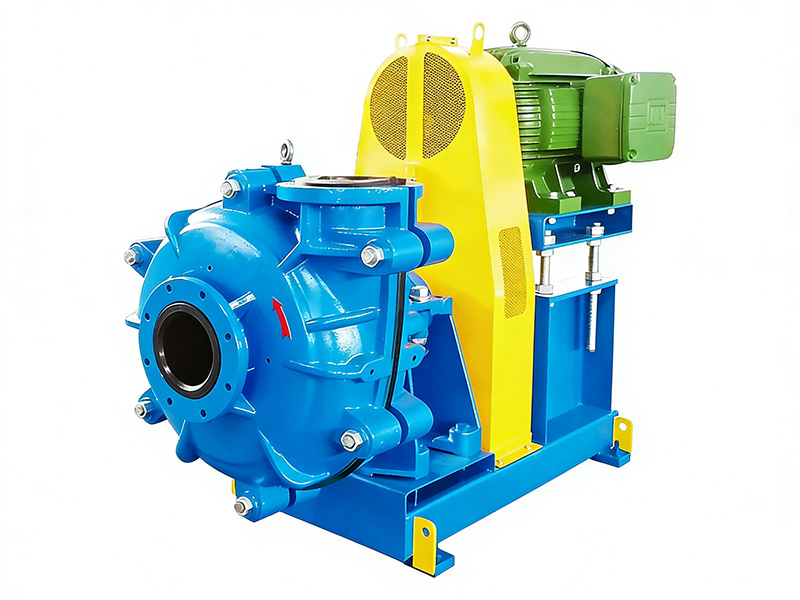
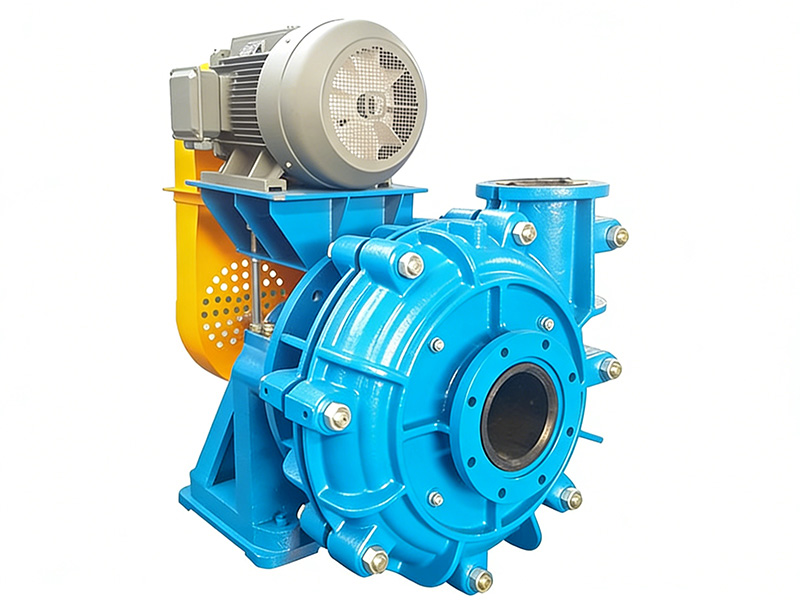
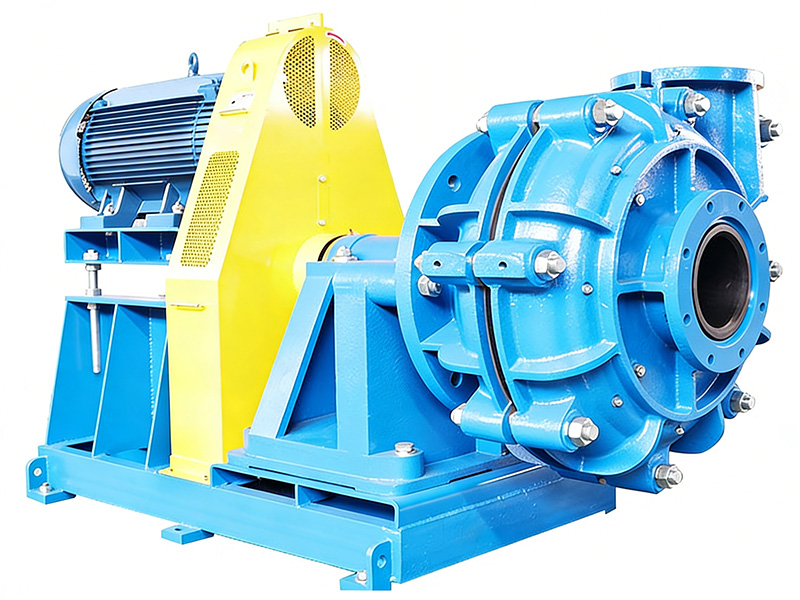
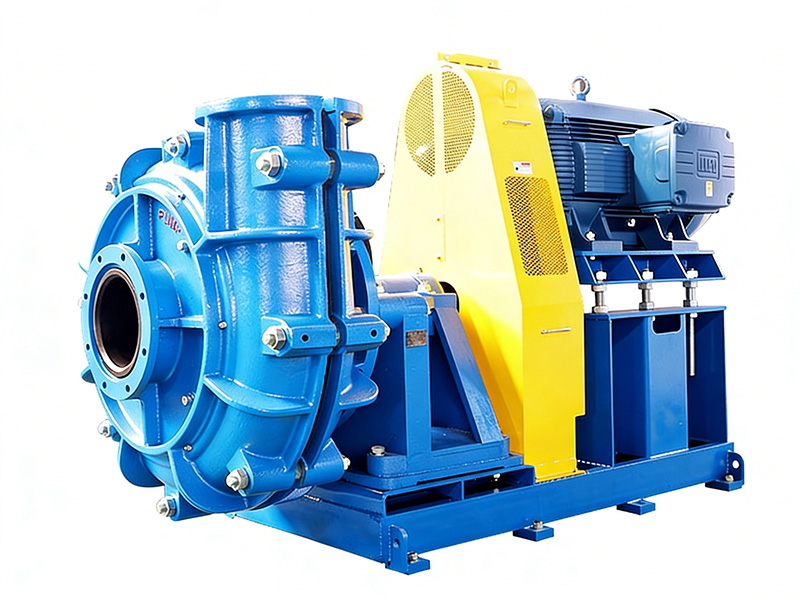
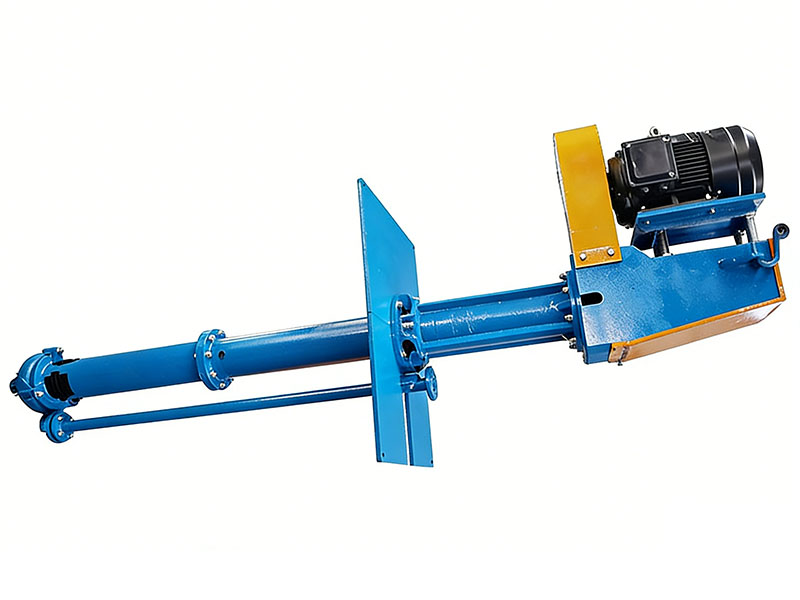
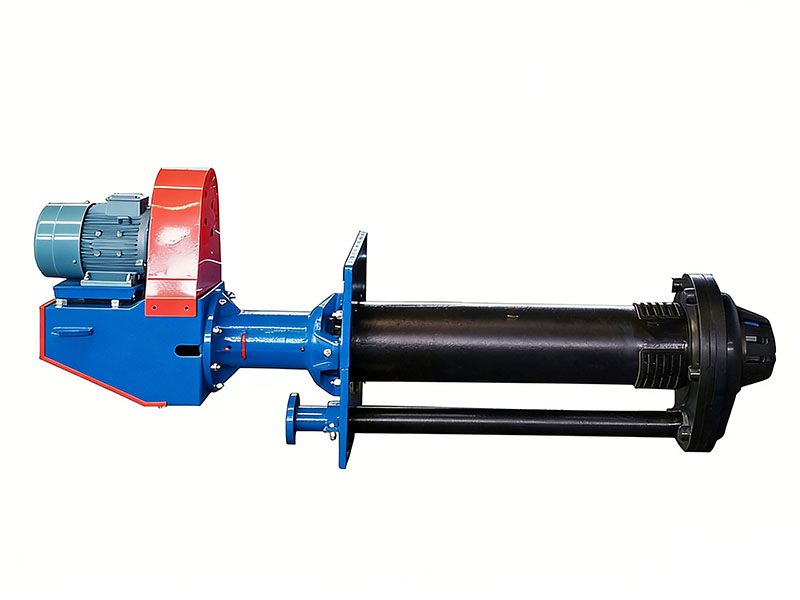
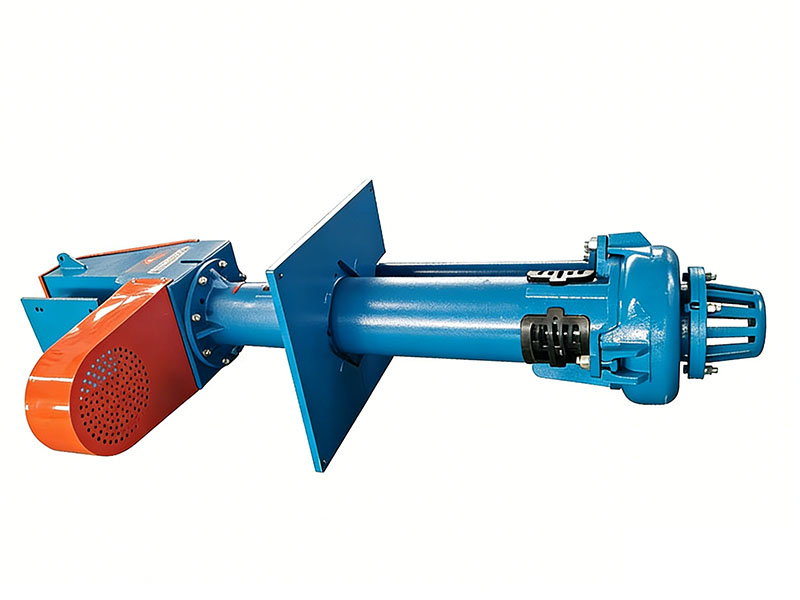
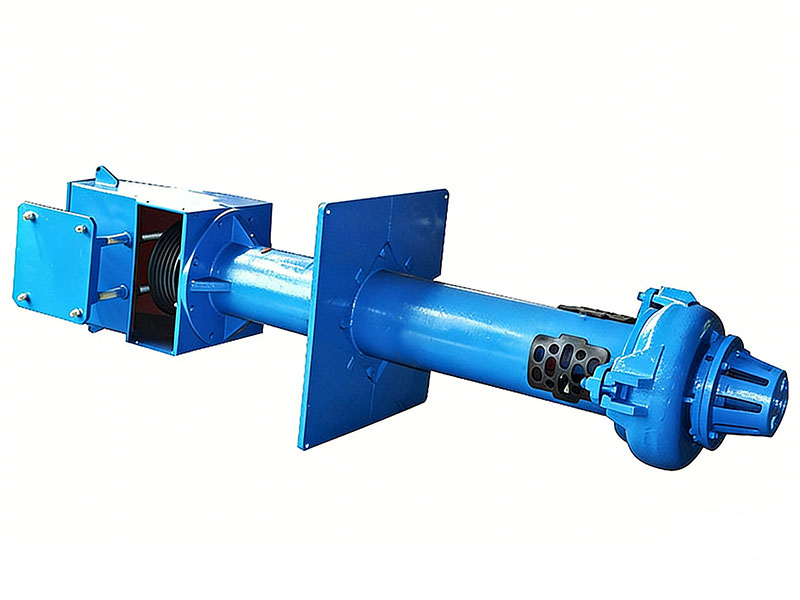
Chemical processing requires pumps capable of handling corrosive, toxic, and high-temperature liquids safely and efficiently. The most commonly used pumps in the chemical industry are chemical centrifugal pumps, magnetic drive pumps, diaphragm pumps, and stainless steel process pumps.
Chemical centrifugal pumps are widely used for transferring acids, alkalis, solvents, and various chemical solutions. Magnetic drive pumps are ideal for leak-free transportation of hazardous liquids. Diaphragm pumps are commonly used for precise dosing and handling viscous or corrosive media.
Chemical pumps are manufactured with corrosion-resistant materials such as stainless steel, fluoroplastic, or special alloys to ensure long service life and safe operation in demanding chemical environments.
Related News
-
Pump knowledge–Introduction to Marine Dredging Pump
Apr26, 2026 -
Knowledge about slurry pumps and water pumps
Apr15, 2026 -
What are the requirements for motor selection of slurry pump
Mar01, 2026 -
Pumps for Limestone-gypsum wet FGD (Flue Gas Desulfurization)
Feb16, 2026 -
Structural Characteristics and Model of ZJ Slurry Pump
Jan27, 2026 -
Knowledge about slurry pumps and water pumps
Jan07, 2026